- Model
- LZS250
- Agitator Power
- 2×55 KW
- Installed Gross Capacity
- ≤155 KW
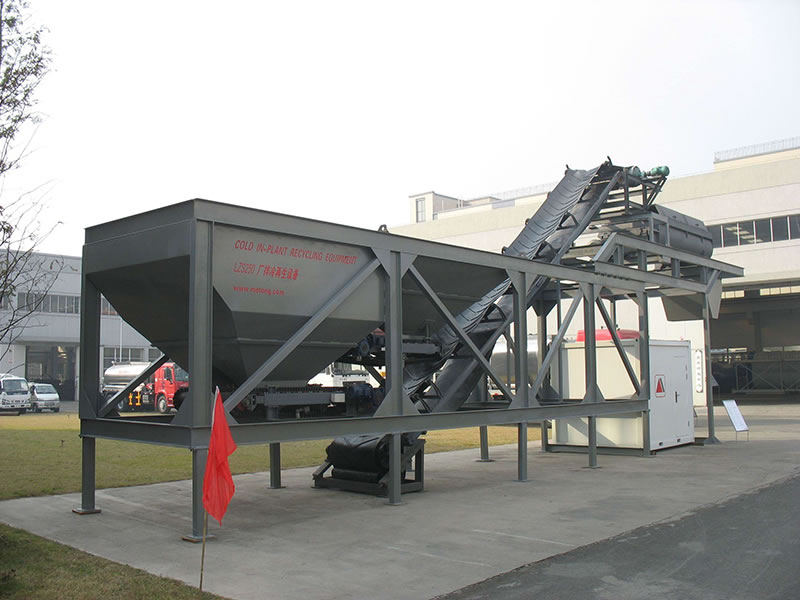
In cold in-plant recycling, the old asphalt pavement material is removed by a milling machine and then transported to a plant where it is crushed, screened, and combined with a certain percentage of new aggregates, asphalt, active fillers and water under normal temperature to form a base course for reconstructed pavement. This technology can not only improve the performance and prolong the service life of asphalt pavement, but also can yield significant savings in materials, thus reducing the project cost. According to a survey undertaken by the U.S. Federal Highway Administration, the asphalt pavement recycling can help save 50% asphalt and reduce 25% pavement construction cost.
Application The cold in-plant recycling equipment can recycle the damaged pavement material and the reclaimed asphalt can be used in the base, sub-base layer of asphalt pavement for expressways, first and second grade highways, as well as the surface layer of asphalt pavement for third and fourth grade highways. After rehabilitation, the road pavement is less liable to crack and can be used for a long time. Functional, economical and eco friendly, our cold in-plant recycling equipment is a product of choice for customers worldwide.
Specifications are model-specific and can be varied for a project. Confirm the final datasheet with engineering before ordering.
The cold in-plant recycling equipment adopts double horizontal shaft high speed boiling agitator, which makes that the oil materials could be thoroughly mixed
It is equipped with dense gear impeller spiral for crushing materials so that the powder could be delivered more accurately
A device for breaking the arch installed at the bottom of the powder hopper makes the powder flow smoothly, thus improving the uniformity of powder delivery
The light-weight and free vibration powder spiral could greatly improve the measurement precision
Intelligent control system with the human-machine interface adopts PLC control and computer measuring controlling display for easy operation to meet the needs of different users
The modular design makes the cold in-plant recycling equipment having the following features such as easy installation, convenient maintenance and quick removal
Specifications
| Specification | Value |
|---|---|
| Model | LZS250 |
| Production | 250 t/h |
| Agitator Power | 2×55 KW |
| Aggregate Hopper | 2×6.5 m3 |
| Powder Hopper | 4 m3 |
| Filling Height | 3.6 m |
| Unloading Height | 3.5 m |
| Installed Gross Capacity | ≤155 KW |
| Operation Mode | Manual/Automatic Control |
Dimensions and capacities are model-specific and may be varied for a project. Confirm the final datasheet with engineering before ordering.
Drawing, configuration options and price on request. Get quote